Introduction
Maintaining consistent product quality is one of the biggest responsibilities in the food manufacturing industry. Every ingredient used in production can influence the safety, taste, shelf life, and overall quality of the final product. Therefore, manufacturers must ensure that their suppliers follow reliable quality practices and meet established food safety requirements.
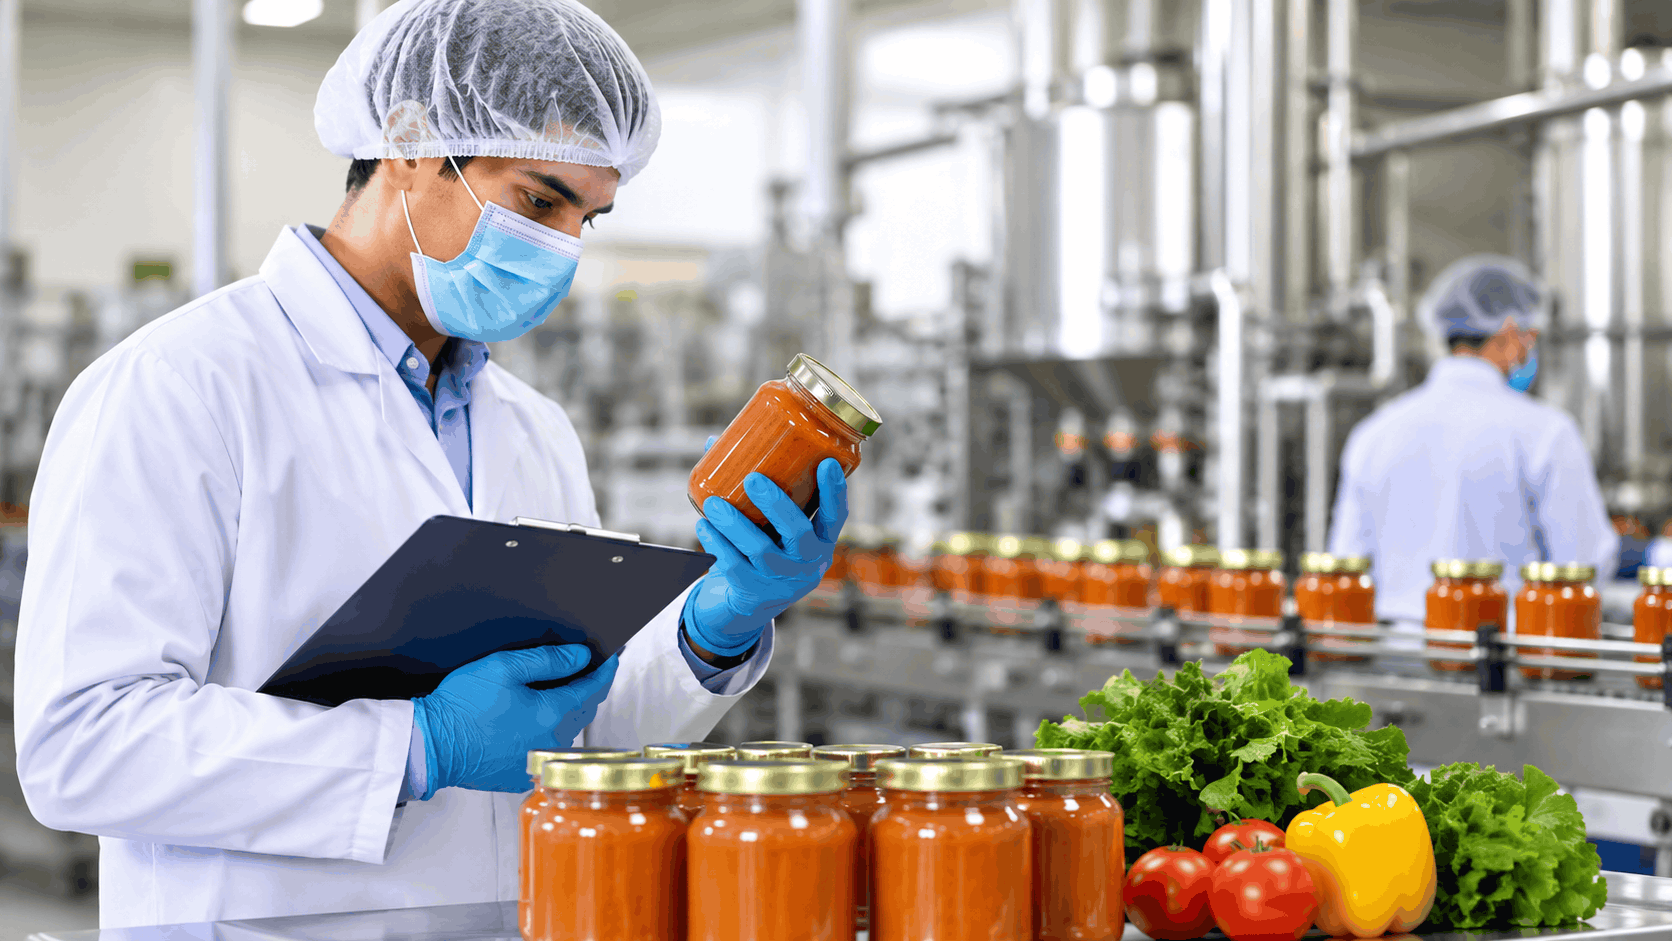
Supplier quality audits play an important role in achieving this objective. They help manufacturers evaluate supplier performance, inspect raw material handling practices, review documentation, and identify potential risks before ingredients enter the production process. In modern food processing, regular supplier assessments are essential for maintaining product consistency, meeting regulatory expectations, and building a dependable food supply chain.
What Are Supplier Quality Audits in Food Manufacturing?
A supplier quality audit is a systematic evaluation of a supplier's facilities, processes, quality management systems, and compliance practices. Its primary purpose is to determine whether suppliers can consistently provide raw materials and packaging components that meet the manufacturer's requirements.
During an audit, manufacturers may examine ingredient sourcing, storage conditions, sanitation procedures, pest control, testing records, traceability systems, and quality documentation. These assessments help identify weaknesses that could affect production or compromise finished-product safety.
Supplier audits can be conducted before establishing a business relationship, at scheduled intervals, or whenever quality concerns arise. Their frequency generally depends on supplier risk, material sensitivity, previous performance, and the potential impact of a quality failure.
Why Supplier Quality Audits Are Important for Food Processing
Strengthening Food Safety Standards
Food safety begins long before ingredients reach the manufacturing facility. Poor handling, unsuitable storage temperatures, contamination, and inadequate sanitation at supplier facilities can introduce risks into the production environment.
Regular supplier audits help identify these issues at an early stage. Manufacturers can evaluate hygiene practices, contamination prevention measures, and handling procedures to ensure that incoming materials meet appropriate safety requirements.
This approach supports preventive food safety management and reduces the possibility of contamination throughout the production process. Manufacturers can also learn more about food safety systems and quality assurance practices that help protect products throughout manufacturing.
Maintaining Consistent Food Quality Control
Variations in raw materials can affect product flavour, texture, appearance, and shelf life. For example, inconsistent ingredient specifications may create noticeable differences between production batches.
Supplier audits help manufacturers verify whether suppliers follow defined quality procedures and maintain consistent material specifications. Reviewing laboratory reports, inspection records, and product testing practices also helps establish greater confidence in incoming materials.
Effective Food Quality Control therefore starts with selecting and monitoring reliable suppliers rather than depending entirely on finished-product inspections. Research and development activities also support product consistency through R&D and Quality Control, including incoming material checks and finished-product verification.
Supporting FSSAI Compliance
Food manufacturers operating in India must pay attention to applicable food safety regulations and requirements established by the Food Safety and Standards Authority of India (FSSAI).
Supplier assessments can help manufacturers review relevant licences, food safety documentation, hygiene practices, and ingredient specifications. They also encourage better record management and traceability throughout the procurement process.
However, supplier audits do not replace statutory inspections or legal compliance responsibilities. Manufacturers must ensure that their own operations and sourcing practices meet applicable regulatory requirements. Reviewing relevant food safety certifications and compliance practices can also help businesses understand the importance of documented food safety systems.
Key Areas Covered During a Supplier Quality Audit
Raw Material Inspection and Documentation
Raw material inspection is one of the most important parts of supplier evaluation. Manufacturers should verify ingredient specifications, certificates of analysis, batch details, expiry information, and relevant testing reports.
These records help confirm that materials meet agreed purchasing requirements. Proper documentation also makes it easier to investigate quality issues and trace affected batches when necessary.
Hygiene and Storage Practices
Suppliers must maintain suitable storage conditions to protect ingredients from moisture, pests, contamination, and other environmental risks. Auditors should examine warehouse cleanliness, stock rotation procedures, temperature monitoring where required, and segregation of different materials.
Evaluating these practices helps manufacturers understand whether ingredients are handled and stored appropriately before transportation.
Supplier Traceability and Corrective Actions
Traceability allows manufacturers to identify where ingredients originated and which production batches used them. Auditors should review supplier records to confirm that materials can be tracked through relevant stages of the supply chain.
When an audit identifies problems, suppliers should provide corrective and preventive action plans. These actions help address the root cause of non-conformities and reduce the possibility of similar issues occurring again.
Benefits of Regular Supplier Quality Audits
Regular supplier audits offer several operational advantages for food manufacturing businesses. They help reduce the risk of receiving unsuitable raw materials, improve supplier accountability, and strengthen relationships between manufacturers and procurement partners.
Another important advantage is improved production consistency. When suppliers follow clearly defined quality requirements, manufacturers can maintain more predictable ingredient specifications and reduce interruptions caused by material-related quality problems.
Supplier assessments also support better risk management. Identifying weaknesses before they affect production can help businesses avoid unnecessary wastage, product rejection, customer complaints, and costly corrective measures.
Furthermore, a structured supplier evaluation programme strengthens Quality Assurance across the entire Food Supply Chain. It encourages transparency, better communication, and continuous improvement among business partners. These principles are also important in EXIITO's food manufacturing operations, where quality standards and food safety discipline guide processes from sourcing to packaging.
Challenges and Future Trends in Supplier Quality Management
Despite their advantages, supplier audits can present practical challenges. Manufacturers working with multiple suppliers may find it difficult to conduct frequent facility inspections, maintain complete documentation, and monitor performance across different locations.
Smaller suppliers may also require additional guidance to understand quality expectations and implement suitable improvement measures. Manufacturers can address these challenges through risk-based audit schedules, clear supplier requirements, regular communication, and documented corrective action procedures.
Technology is also changing supplier quality management. Digital documentation systems, automated monitoring tools, and traceability platforms are making it easier to maintain records and review supplier performance. Data-driven assessments can help manufacturers identify recurring quality issues and prioritise suppliers that require additional attention.
In the coming years, stronger traceability, digital supplier evaluation, and preventive quality management are likely to become increasingly important for businesses seeking reliable and transparent food manufacturing operations.
Conclusion and CTA
Supplier quality audits are an essential part of maintaining food manufacturing standards. By evaluating raw material quality, hygiene practices, documentation, traceability, and regulatory compliance, manufacturers can identify potential risks before they affect finished products.
A well-managed supplier audit programme strengthens Food Safety, improves Food Quality Control, and supports consistent production. Rather than treating audits as occasional inspections, businesses should consider them an ongoing part of their Quality Assurance strategy.
Looking for a reliable food manufacturing partner? Explore EXIITO Beverages, a premium food manufacturing company offering beverages, namkeen, makhana, and pickles, along with private label and other manufacturing solutions. Visit our website to explore our manufacturing capabilities and discuss your business requirements.