
Introduction
Makhana, also known as fox nuts or lotus seeds, has become an increasingly popular snack in India's packaged food industry. Its light texture, versatility and ability to absorb different flavours make it suitable for various snack applications. As consumer expectations for food quality and safety continue to grow, manufacturers must maintain consistent production standards through appropriate inspection and testing procedures.
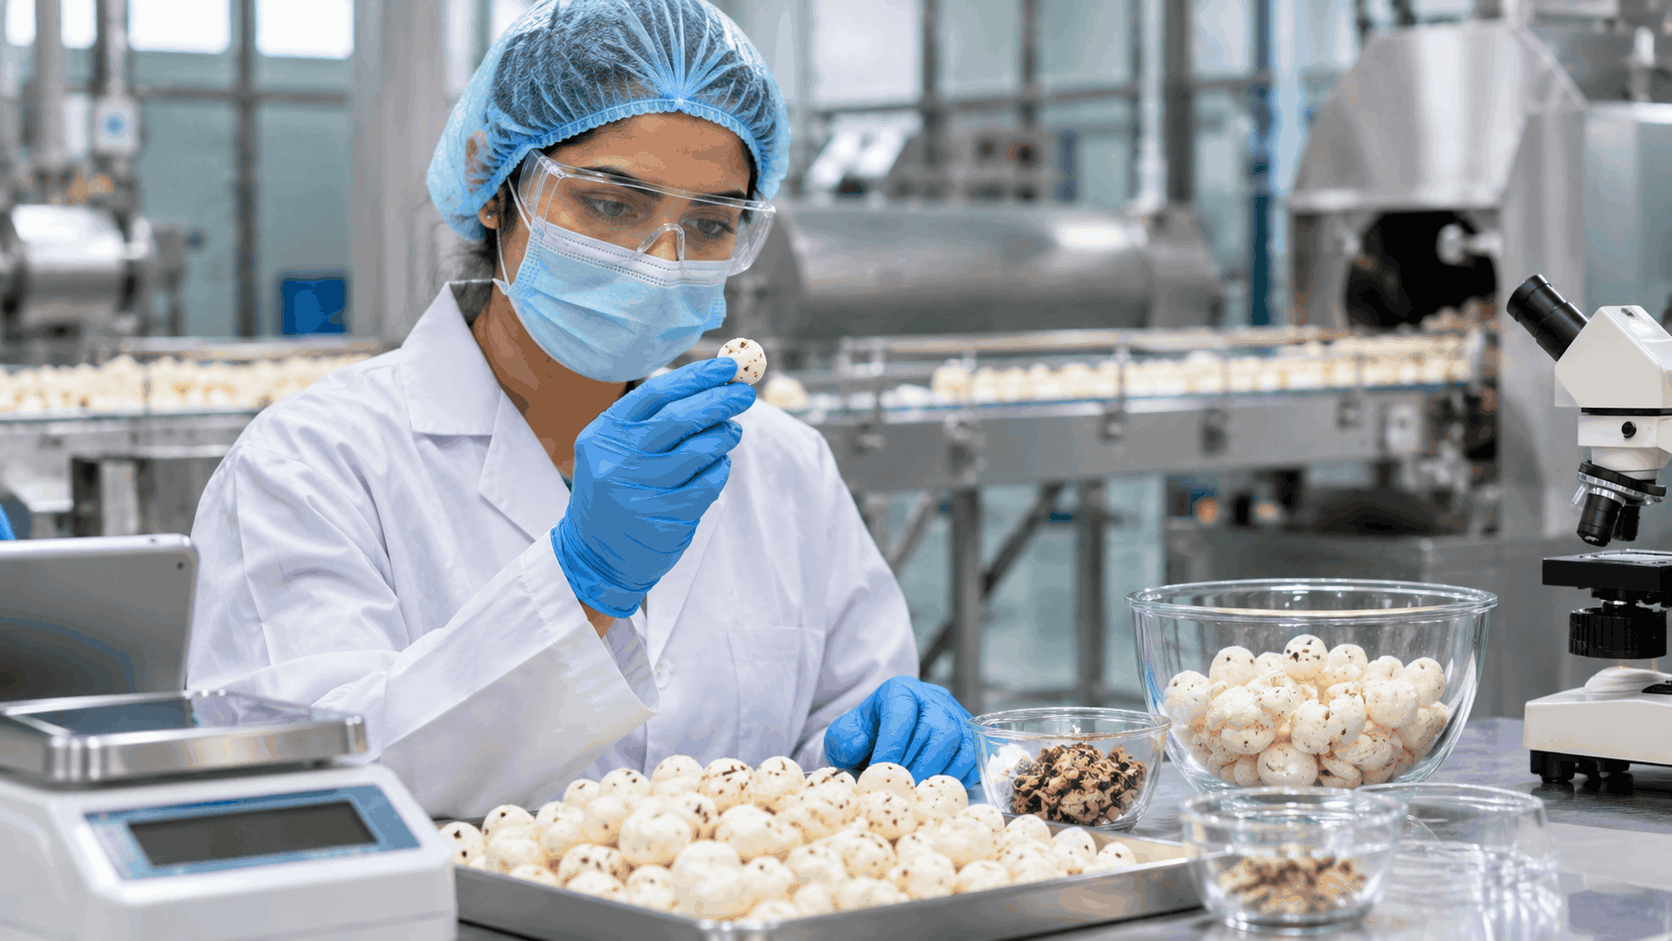
Quality Testing in Makhana Manufacturing plays an important role in ensuring that finished products meet established quality and safety requirements. From inspecting incoming raw materials to evaluating roasted, seasoned and packaged makhana, every production stage requires suitable quality checks. Effective testing helps manufacturers identify defects, maintain product consistency and deliver reliable products to consumers.
Understanding Makhana Quality Control in Manufacturing
Makhana Quality Control involves monitoring raw materials, processing conditions and finished products to maintain consistent quality. It includes physical inspection, sensory evaluation, moisture assessment, hygiene monitoring and packaging verification.
The primary objective is to identify potential quality issues before products reach consumers. Manufacturers establish product specifications and inspection procedures according to the product type, processing requirements and applicable food safety regulations.
For manufacturers producing different varieties, such as flavoured makhana, maintaining consistent texture, seasoning distribution and overall appearance is particularly important. You can explore EXIITO's Makhana Product Range to understand the different flavour varieties available in the market.
Key Quality Testing Methods Used in Makhana Manufacturing
Raw Material Inspection
Quality testing begins with inspecting incoming makhana before processing. Manufacturers examine raw materials for visible impurities, damaged pieces, discolouration and unwanted foreign particles.
The size, appearance and overall condition of the seeds are also evaluated against approved specifications. Proper raw material inspection helps prevent unsuitable ingredients from entering the production process and supports better finished-product consistency.
Moisture Content Testing
Moisture content is an important quality parameter in makhana manufacturing because it influences texture, crispness and storage stability.
Manufacturers can use suitable moisture analysers or laboratory methods to assess moisture levels. Testing helps identify products that may require additional drying or processing adjustments.
Maintaining an appropriate moisture level is essential for achieving the desired crisp texture and reducing quality deterioration during storage. Acceptable moisture limits should be established according to product specifications and applicable requirements.
Physical Appearance and Size Inspection
Physical inspection helps manufacturers evaluate the appearance and uniformity of makhana. Samples are examined for broken pieces, excessive dark spots, uneven shapes and visible defects.
Size grading may also be performed to maintain consistency within production batches. Uniform appearance is particularly important for premium snack products because it contributes to product presentation and consumer acceptance.
Texture and Sensory Evaluation
Sensory evaluation is another important part of Makhana Quality Control. Trained evaluators assess characteristics such as crispness, flavour, aroma, colour and overall acceptability.
Texture evaluation helps determine whether the product delivers the expected crunch. For flavoured varieties, evaluators also check seasoning distribution, flavour intensity and consistency.
Different seasoning profiles require attention to both flavour and texture. For example, EXIITO Mexican Makhana and Himalayan Salt & Turmeric Makhana represent different flavour combinations that require suitable product evaluation.
For additional information about ingredient selection and flavour development, read our related article on Makhana Ingredients and Seasonings: Exploring Flavour Innovation in Healthy Snacks.
Foreign Matter and Contamination Inspection
Foreign matter inspection helps identify unwanted materials that could affect product safety and quality. Depending on the manufacturing setup, inspection may involve visual examination, sieving and suitable screening equipment.
Metal detection or other appropriate detection systems may also be used as part of a manufacturer's food safety programme. Equipment selection and inspection frequency should be based on product risks and the established control plan.
Maintaining clean processing areas, suitable equipment hygiene and proper employee practices further supports contamination prevention. Manufacturers should also establish suitable cleaning and sanitation procedures to minimise contamination risks.
Microbiological Testing
Microbiological testing helps evaluate the hygienic quality and safety of food products. Depending on the product, ingredients, processing conditions and regulatory requirements, manufacturers may conduct laboratory testing for relevant microorganisms.
Testing parameters should be selected according to applicable food safety standards and the product's risk assessment. Appropriate sampling, laboratory procedures and documented results help manufacturers determine whether products meet established microbiological specifications.
Regular monitoring and documented testing procedures also support an organised quality management system.
Packaging Inspection and Finished Product Testing
Quality inspection does not end after processing. Packaging is another important stage because it protects makhana from moisture, physical damage and external contamination.
Manufacturers inspect packaging materials for suitability, cleanliness and structural integrity. They also verify sealing quality, net weight, labelling information, batch identification and applicable manufacturing and expiry date markings.
Finished-product samples may undergo storage and shelf-life evaluation under defined conditions. These assessments help manufacturers understand changes in crispness, flavour, appearance and packaging performance over time.
Proper packaging inspection helps maintain the intended product characteristics throughout distribution and storage.
Importance of Research and Quality Control in Makhana Manufacturing
Research and development work alongside quality control to improve product formulations, processing conditions and finished-product consistency.
Manufacturers can use sensory evaluations, process trials and quality assessments to refine flavour profiles and production specifications. Documented inspections also help identify variations between batches and support continuous improvement.
At EXIITO, the R&D and Quality Control process connects product development with incoming material checks, in-process monitoring, finished-goods inspection and traceability records.
A structured approach to research and quality management helps manufacturers maintain consistency while developing new products and expanding their product portfolios.
Challenges and Future Trends in Makhana Quality Testing
Maintaining consistent quality can be challenging when raw material characteristics, processing conditions and seasoning requirements vary between batches. Inadequate moisture control, inconsistent roasting and unsuitable packaging can also affect finished-product quality.
Modern manufacturing is increasingly incorporating improved inspection equipment, digital quality records and standardised testing procedures. These approaches can help manufacturers identify variations earlier, improve traceability and make production decisions using documented information.
As the packaged makhana market develops, manufacturers may also explore more advanced testing methods, automated inspection systems and improved shelf-life evaluation techniques to strengthen quality management.
Conclusion
Quality Testing in Makhana Manufacturing is essential for maintaining product consistency, food safety and consumer confidence. From raw material inspection and moisture assessment to sensory evaluation, microbiological testing and packaging verification, every quality checkpoint contributes to the final product.
Effective Makhana Quality Control requires a structured approach that combines suitable testing procedures, hygienic manufacturing practices and documented quality checks. Continuous monitoring and process improvement can help manufacturers meet product specifications and maintain reliable quality standards.
Explore Makhana Manufacturing Opportunities with EXIITO
EXIITO focuses on quality-oriented food manufacturing across categories such as beverages, namkeen, makhana and pickles. Our product development and quality management approach supports own-brand products and manufacturing partnerships.
Explore our Makhana Product Range and learn more about our R&D and Quality Control capabilities.
Are you planning to introduce your own makhana snack brand? Discover our Private Label and ODM Manufacturing Solutions or contact EXIITO to discuss your product and manufacturing requirements.